The cheapest cutting process is not always the fastest machine. Laser cutting, turret punching and hard-tool stamping solve different geometry and volume problems.
Short answer
- Choose fiber laser cutting for prototypes, changing designs, complex outlines, tight nesting and low-to-medium volume.
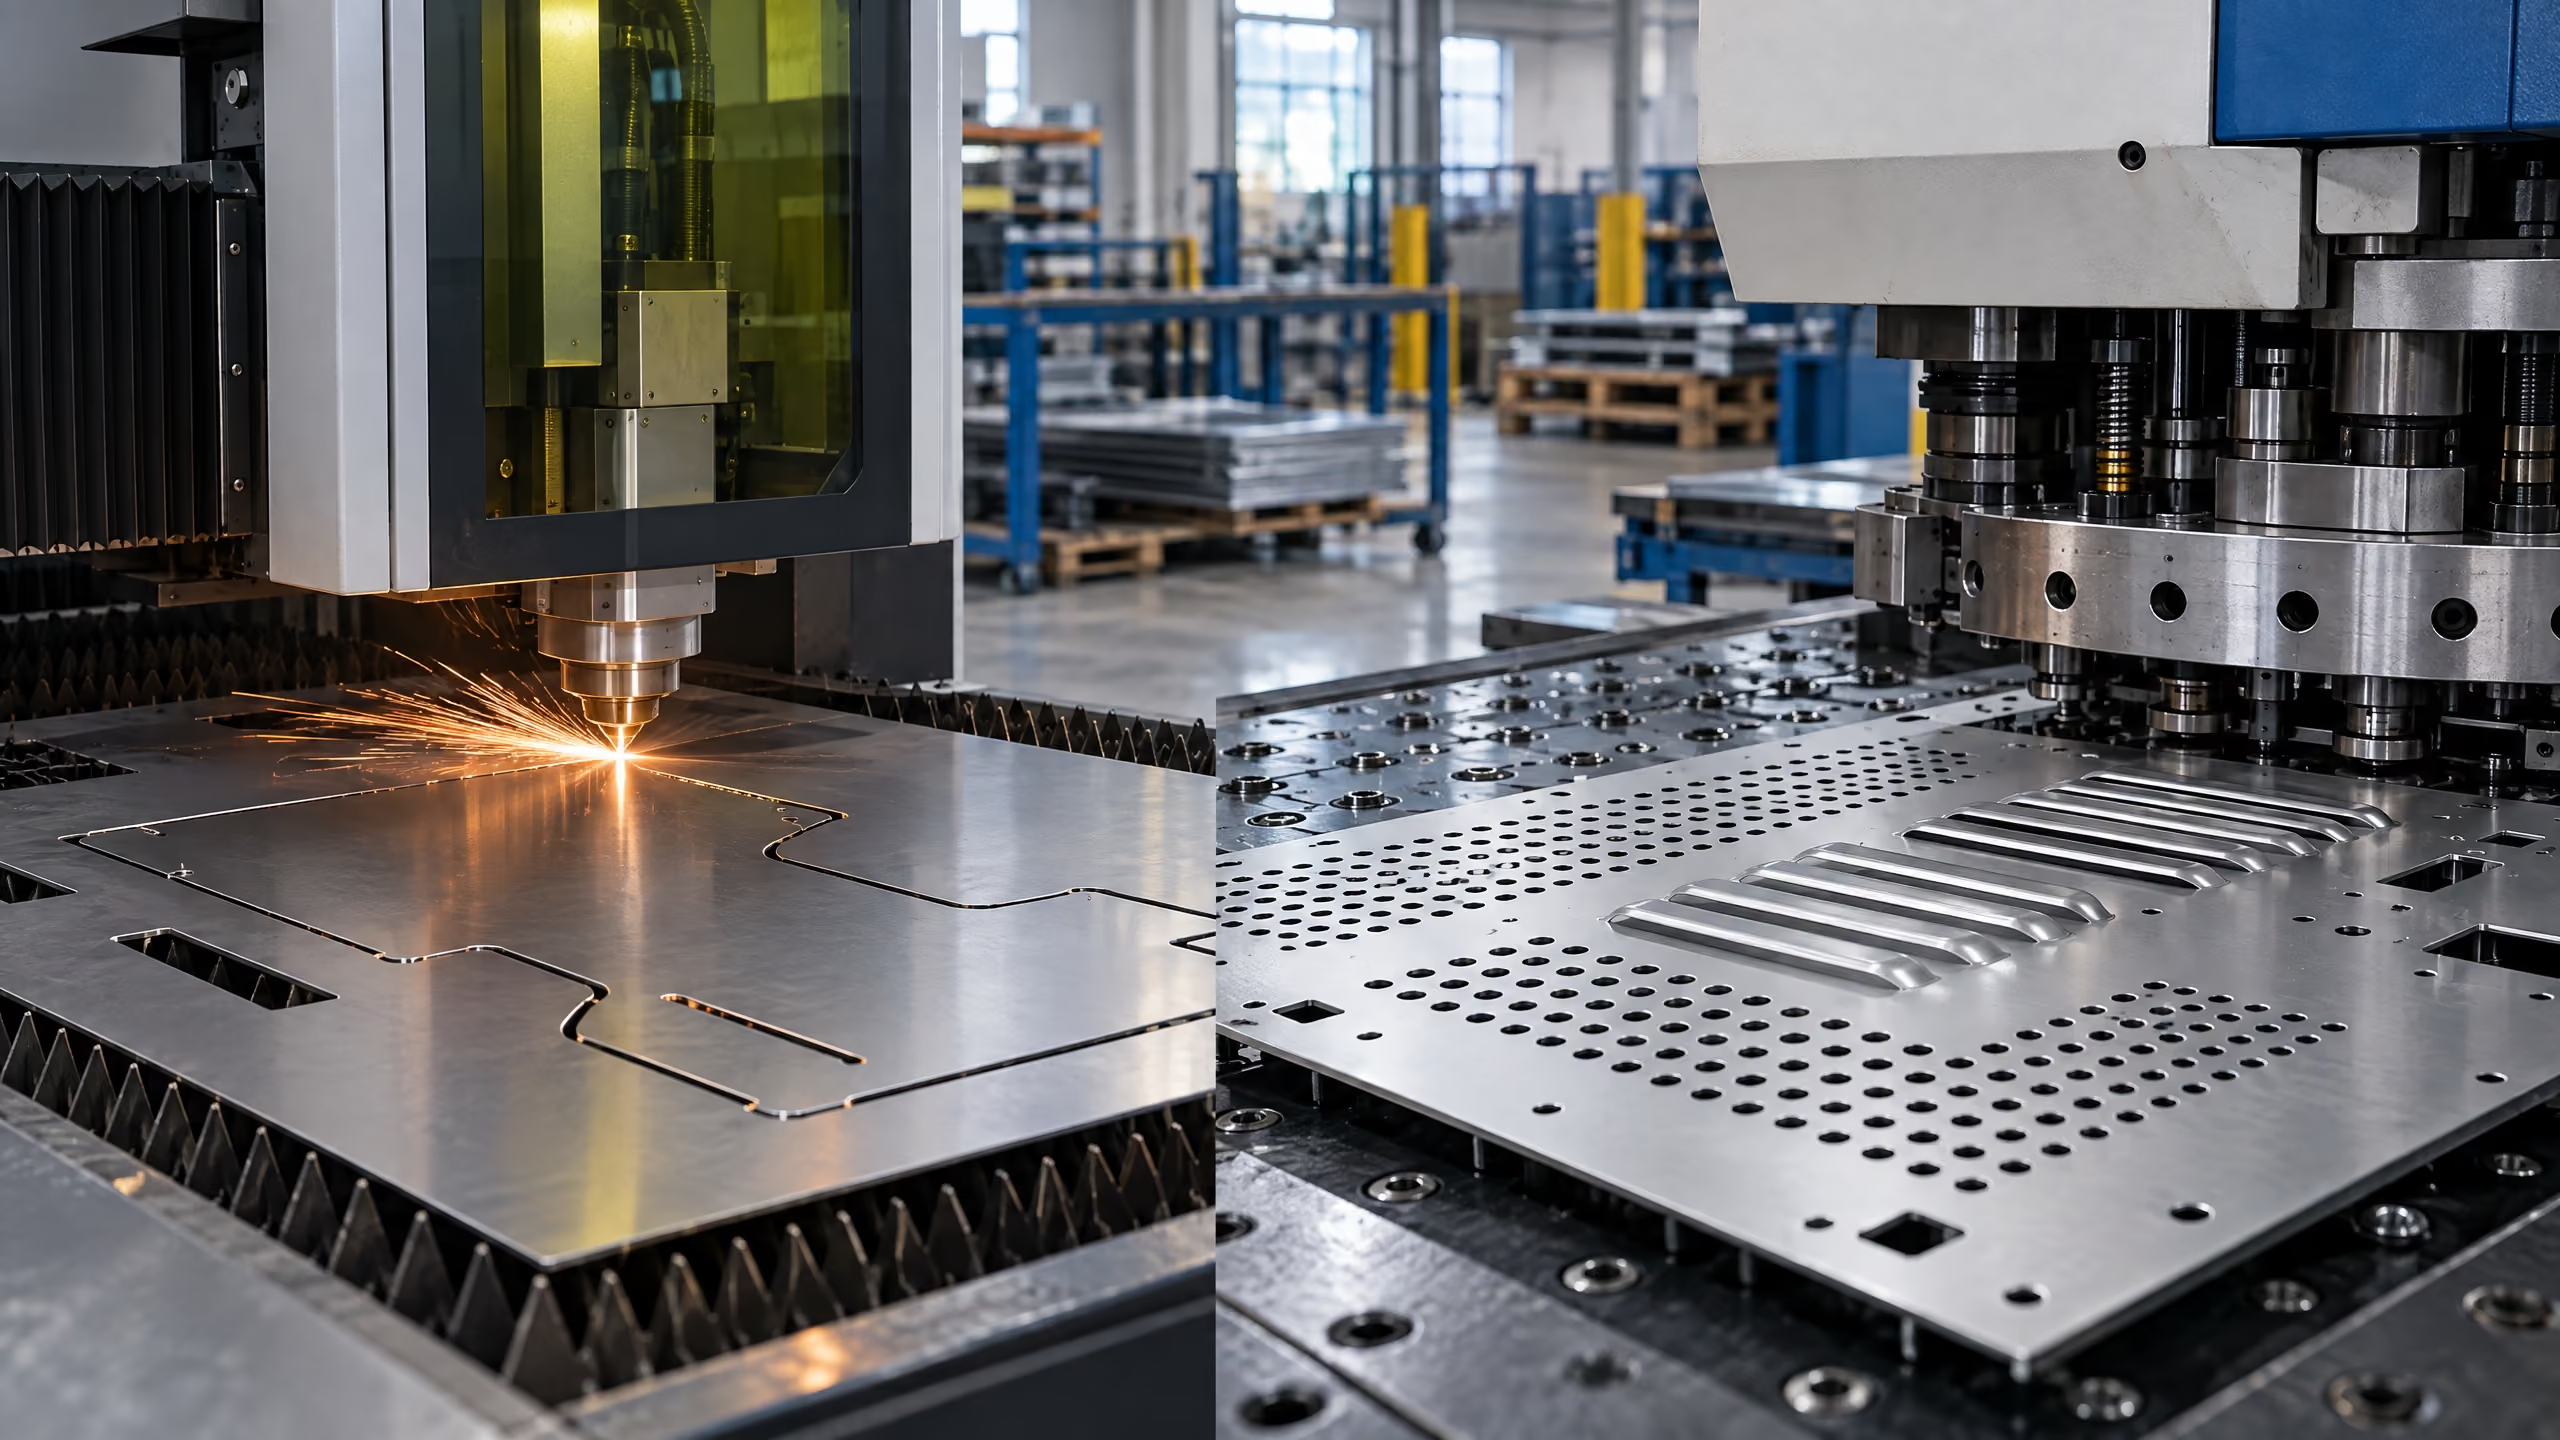
- Choose turret punching for hole-dense panels and parts that need louvers, dimples, countersinks or other formed features.
- Consider hard tooling only when annual volume and design stability justify the tooling cost.
Compare the real cost drivers
| Cost driver | Fiber laser | Turret punch |
|---|---|---|
| Setup | Very low | Low, but tool selection matters |
| Complex outlines | Excellent | Limited by tool geometry |
| Hundreds of holes | Slower per hole | Usually faster |
| Formed features | Separate operation | Can run in the machine |
| Design changes | Easy | Tooling or program changes |
| Best volume | Prototype to medium | Medium to high |
Material utilization can change the answer. A laser can nest irregular parts tightly across a sheet, while a turret may use regular punch patterns and common tooling. Always compare the complete routed cost, not only machine time.
When turret punching wins
A ventilation panel with 600 identical holes is a typical turret-punch part. The machine can punch a regular pattern quickly and form louvers or countersinks without moving the part to another press.
Turret punching also becomes attractive when the same geometry repeats across a stable product family and the tool library already covers the required features.
When laser cutting wins
Prototype enclosures, brackets and one-off replacement parts usually belong on the laser. There is no hard tool to buy, the program changes in minutes, and the cut edge is ready for bending after normal deburring.
For stainless and aluminum designs with changing hole positions, laser cutting also removes the risk of building the quotation around a tool that may not fit the next revision.
What to send for an accurate comparison
Send a DXF or STEP file, material, thickness, quantity, surface finish and tolerance callouts. If the part has louvers, countersinks or embossed features, mark them clearly. A good fabricator will then compare laser, turret and tooling routes and explain the cost difference.
Rule of thumb: use laser cutting to prove the design, turret punching to optimize a stable design, and hard tooling only when volume makes the payback obvious.